English
 Español
 Русский
 لالعربية
explosion proof ribbon mixer chemical industry Comparison: In-Depth Analysis of Features, Performance, and Applications
release time:
2026-06-17
Detailed comparison of explosion proof ribbon mixer chemical industry technologies. Analyze features, performance metrics, and application scenarios including chemical resistant ribbon mixer materials, hazardous material mixing safety protocols, and corrosion resistant ribbon mixer design. Make informed decisions with our expert analysis.
explosion proof ribbon mixer chemical industry Comparison: In-Depth Analysis of Features, Performance, and Applications Comparative analysis of different explosion proof ribbon mixer chemical industry technologies and their applications..
This comprehensive guide provides in-depth analysis, practical insights, and expert recommendations for explosion proof ribbon mixer chemical industry..
Whether you're a plant manager, engineer, or procurement specialist, you'll find valuable information to optimize your operations..
Comparison Methodology and Criteria Explanation of comparison criteria, evaluation methods, and scoring system..
Feature Comparison: chemical resistant ribbon mixer materials Comparison: Detailed feature comparison table for chemical resistant ribbon mixer materials Feature Option A Option B Option C Recommendation Performance Analysis: hazardous material mixing safety protocols Performance metrics and analysis for hazardous material mixing safety protocols with test results..
Cost-Benefit Analysis: corrosion resistant ribbon mixer design Economic analysis including initial costs, operating expenses, and ROI calculations..
Application Suitability: chemical mixer ventilation requirements Key Points: Application scenarios and suitability assessment for chemical mixer ventilation requirements Technical Specifications: explosion protection for industrial mixers Comparison: Technical specification comparison for explosion protection for industrial mixers Feature Option A Option B Option C Recommendation User Experience: chemical mixing risk assessment User experience evaluation including ease of use, maintenance, and support..
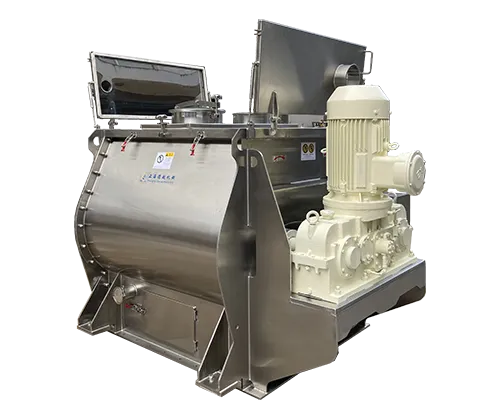
Ribbon mixers are essential equipment in various industrial applications, particularly in the food, pharmaceutical, and chemical industries. The unique ribbon blade design creates both axial and radial mixing motions, ensuring homogeneous blending of dry powders and granular materials.
The explosion proof ribbon mixer chemical industry Comparison features a dual-ribbon agitator that moves materials in opposite directions simultaneously. This design promotes efficient mixing while minimizing product degradation and heat generation, making it ideal for sensitive materials.
When selecting a ribbon mixer for explosion proof ribbon mixer chemical industry Comparison applications, consider factors such as material characteristics, batch size requirements, and sanitary design specifications. Proper equipment selection ensures optimal mixing performance and product quality consistency.
Key Benefits and Advantages of explosion proof ribbon mixer chemical industry Comparison:
- Gentle mixing action – preserves particle integrity and prevents material degradation
- Uniform blending – ensures consistent product quality throughout the batch
- Efficient discharge – complete emptying with minimal residue retention
- Versatile applications – suitable for dry powders, granules, and cohesive materials
- Easy maintenance – accessible design for cleaning and component replacement
Technical Specifications and Features:
- Capacity range – from laboratory scale to industrial production volumes
- Construction materials – stainless steel, carbon steel, or specialty alloys
- Drive systems – variable speed controls with torque monitoring
- Sealing options – mechanical seals, packing glands, or magnetic drives
- Discharge mechanisms – slide gates, butterfly valves, or pneumatic doors
- Control systems – manual, semi-automatic, or fully automated operation
- Safety features – emergency stops, interlocks, and guarding systems
Applications and Industry Use Cases:
- Food industry – blending dry ingredients, spices, and food additives
- Pharmaceuticals – mixing active ingredients with excipients
- Chemicals – combining powders, granules, and catalyst materials
- Construction materials – cement, mortar, and dry mix formulations
- Plastics and polymers – compounding additives and colorants
- Agriculture – fertilizer blending and seed treatment formulations
- Cosmetics – powder blending for makeup and personal care products
Selection Criteria and Considerations:
1. Material characteristics including particle size, density, and flow properties
2. Required mixing intensity and homogeneity specifications for the application
3. Batch size requirements and production capacity considerations
4. Sanitary requirements and cleanability specifications
5. Available installation space and utility connections
6. Maintenance accessibility and service requirements
7. Budget constraints and return on investment calculations
Best Practices for Optimal Performance:
1. Conduct material testing to determine optimal mixing parameters
2. Implement regular maintenance schedules for seals, bearings, and drives
3. Train operators on proper loading, mixing, and discharge procedures
4. Monitor mixing performance through regular sampling and analysis
5. Document all maintenance activities and performance observations
6. Stay informed about technological advancements and upgrade opportunities
7. Establish quality control procedures for consistent product quality
Future Trends and Developments: The mixing equipment industry is evolving with advancements in automation, IoT integration, and sustainable technologies. Future explosion proof ribbon mixer chemical industry Comparison systems will incorporate smart sensors for real-time process monitoring, predictive maintenance algorithms, and energy optimization features. Digital twin technology and advanced simulation software are transforming equipment design and optimization processes, enabling virtual testing and performance prediction before physical implementation.
For comprehensive technical consultation, equipment selection guidance, and professional support regarding explosion proof ribbon mixer chemical industry Comparison implementation, please contact our expert engineering team. We provide customized solutions tailored to your specific application requirements, operational objectives, and quality standards. Our technical specialists can assist with equipment specification, process optimization, and implementation strategies to ensure successful integration into your production environment.
label:
related news