English
 Español
 Русский
 لالعربية
Food Grade Ribbon Mixer: The Complete Guide to Hygienic Powder Blending for Food Processing
release time:
2026-06-27
In the food processing industry, maintaining strict hygiene standards while achieving uniform powder blending is non-negotiable. A food grade ribbon mixer is pu
Food Grade Ribbon Mixer: The Complete Guide to Hygienic Powder Blending for Food Processing

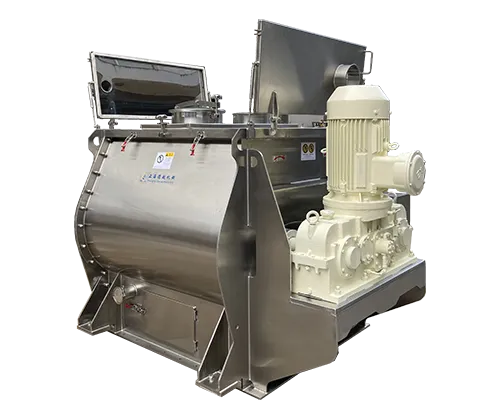
In the food processing industry, maintaining strict hygiene standards while achieving uniform powder blending is non-negotiable. A food grade ribbon mixer is purpose-built to meet these demands, combining sanitary design principles with efficient mixing performance. Whether you are producing flour blends, spice mixes, protein powders, or milk powder formulations, understanding the capabilities and specifications of a food-grade ribbon mixer is essential for ensuring product safety, regulatory compliance, and operational efficiency.
Shanghai Deyue Machinery has been manufacturing and exporting food grade ribbon mixers to markets worldwide, including Spain, Russia, and Arab food processing facilities. Our machines are constructed from SS304 and SS316L stainless steel, equipped with CIP clean-in-place systems, and designed for fully dust-free operation — meeting the most demanding food safety standards.
Why Food Grade Ribbon Mixers Are Essential in Food Processing
Ribbon blenders have long been the workhorse of dry powder mixing across industries. However, when applied to food production, standard ribbon mixers fall short because they lack the hygienic features required by food safety regulations. A food grade mixer SS304 addresses every concern — from material compatibility to cleanability — making it the preferred choice for food manufacturers globally.
The core advantage lies in the double helical ribbon agitator design. The inner ribbon pushes material inward while the outer ribbon pushes it outward, creating a continuous convective mixing pattern. In food applications, this ensures thorough homogenization of ingredients with vastly different densities — such as blending fine salt with coarse sugar crystals or incorporating trace additives into bulk protein powder.
Beyond mixing efficiency, a proper food grade ribbon mixer eliminates contamination risks. All product-contact surfaces are fabricated from food-grade stainless steel, polished to a smooth finish that prevents bacterial adhesion. Sealed bearings, sanitary gaskets, and dust-tight enclosures ensure zero cross-contamination between batches.
Construction Standards: SS304 and SS316L Stainless Steel
The material specification of a sanitary mixer defines its suitability for food processing. Shanghai Deyue Machinery uses only certified food-grade stainless steel for all product-contact components.
SS304 Stainless Steel is the standard material for most food applications. It offers excellent corrosion resistance against common food acids, is non-reactive with acidic or alkaline ingredients, and maintains structural integrity during repeated cleaning cycles. SS304 ribbon mixers are ideal for dry goods such as flour, sugar, baking powder, and spice blends.
SS316L Stainless Steel provides enhanced corrosion resistance due to its molybdenum content. This makes it the preferred choice for applications involving saline environments, dairy products, or highly acidic formulations. A milk powder mixer operating in wet-spray applications benefits significantly from SS316L construction, which resists chloride-induced pitting far better than SS304.
| Specification | SS304 Food Grade Mixer | SS316L Sanitary Mixer |
|---|---|---|
| Corrosion Resistance | Good — standard food acids | Excellent — saline, dairy, acidic |
| Surface Finish | SRA 0.4–0.8 μm (Ra) | SRA ≤0.4 μm (Ra) electropolished |
| Typical Applications | Flour, sugar, spices, protein powder | Milk powder, dairy blends, sauces |
| Temperature Range | -40°C to 300°C | -40°C to 350°C |
| Regulatory Compliance | EU 1935/2004, FDA 21 CFR | EU 1935/2004, FDA 21 CFR, EHEDG |
CIP Clean-in-Place Systems for Food Grade Ribbon Mixers
Cleanliness is the cornerstone of food safety. Manual cleaning of industrial mixers is labor-intensive, inconsistent, and poses contamination risks. A CIP mixer solves these problems by automating the entire cleaning cycle without disassembly.
Our food grade ribbon mixers integrate permanent spray balls and rotating jet nozzles positioned at strategic points inside the mixing vessel. During a CIP cycle, cleaning solution — typically hot water, caustic soda, or acid wash — is circulated through the nozzles at controlled pressure and temperature. The solution reaches every interior surface, dissolving residue and flushing it out through the discharge valve.
A typical CIP cycle for a food grade ribbon mixer includes five stages:
- Pre-rinse: Warm water flush removes loose particulate matter and residual product.
- Caustic wash: Hot alkaline solution at 60–80°C breaks down organic residues, fats, and proteins.
- Intermediate rinse: Deionized or purified water removes all detergent traces.
- Acid wash: Mild acid solution at pH 2–3 eliminates mineral deposits and inorganic scaling.
- Final rinse: Sterile water prepares the vessel for the next production batch.
The entire automated process takes approximately 45 to 90 minutes depending on vessel size and soil level. Operators simply program the cycle parameters through a PLC touchscreen interface — no manual scrubbing or component removal required. This dramatically reduces water and chemical consumption while delivering a consistently validated clean surface.
Dust-Free Operation and Environmental Control
Powder handling in food manufacturing presents a significant dust hazard. Airborne flour particles, spice dust, and protein powder fines not only create explosive atmospheres but also contaminate surrounding equipment and compromise worker health. A food grade ribbon mixer from Shanghai Deyue incorporates multiple dust containment features:
- Sealed lid design: A pneumatically operated or quick-release clamp ring secures the top cover with a food-grade silicone gasket, preventing dust escape during mixing.
- Vacuum-assisted discharge: Product is drawn through a sealed connection to downstream packaging lines, eliminating open transfer points where dust could逸散.
- Dust port with bag filter: A dedicated vent fitted with a HEPA-rated bag filter captures fine particles and returns them to the mixture, maintaining a closed-loop system.
- Negative pressure operation: Optional integrated exhaust fans maintain slight negative pressure inside the vessel, ensuring any potential leakage flows inward rather than outward.
These features make our ribbon mixers suitable for spice mixer industrial applications where aromatic compounds must be contained, as well as for protein powder and milk powder facilities where fine particle dispersion is a major concern.
Food Industry Applications
Food grade ribbon mixers are versatile enough to handle a wide spectrum of dry and semi-dry food ingredients. Below is a comprehensive overview of common applications:
| Application | Ingredients Mixed | Recommended Configuration |
|---|---|---|
| Flour & Baking Blends | Wheat flour, baking powder, salt, sugar | SS304, 1–5 ton/hr, CIP capable |
| Spice & Seasoning | Spices, MSG, flavor enhancers, anti-caking agents | SS304/SS316L, dust-tight seal, vacuum discharge |
| Protein Powder | Whey protein, casein, amino acids, maltodextrin | SS316L electropolished, low-shear ribbon, CIP |
| Milk Powder | Dried whole milk, skim milk, formula bases | SS316L, CIP mixer, explosion-proof motor |
| Sugar & Sweeteners | Granulated sugar, fructose, stevia blends | SS304, polished interior, gentle agitation |
| Dry Soup & Sauce Mixes | Dehydrated vegetables, starch, seasoning packets | SS304, 2–10 ton/hr, quick-discharge valve |
| Nutritional Supplements | Vitamins, minerals, probiotics, fiber blends | SS316L, validated cleaning, GMP-certified |
For large-scale food production facilities, our DLH Large Scale Ribbon Mixer series handles capacities from 1,000 liters to 10,000 liters per batch, making it ideal for commercial bakeries, dairy processors, and multinational spice manufacturers.
Key Technical Specifications
Shanghai Deyue food grade ribbon mixers are engineered to deliver consistent performance across diverse food processing environments. Standard configurations include:
- Capacity range: 100 L to 10,000 L per batch
- Mixing time: 3 to 15 minutes per batch (depending on formulation)
- Motor power: 2.2 kW to 55 kW (variable frequency drive standard)
- Ribbon speed: 20–60 RPM adjustable
- Discharge mechanism: Bottom butterfly valve or ball valve, fully sealed
- Power supply: 380V/50Hz standard; 440V/60Hz available for export markets
- Control system: Siemens or ABB PLC with HMI touchscreen
- Seal type: Double mechanical seal or magnetic drive seal (zero-leakage)
All units undergo rigorous factory acceptance testing, including a water-tightness test, motor amperage verification, and mixing uniformity validation using tracer methods. Certifications available include CE, ISO 9001, and GMP compliance documentation.
Export Experience: Serving Global Food Markets
Shanghai Deyue Machinery has extensive experience exporting food grade ribbon mixers to international food processing markets. Our installations include:
- Spain: Multiple spice processing plants in Andalusia and Catalonia use our SS304 ribbon mixers for paprika, saffron, and seasoning blend production. The mixers comply with EU hygiene directives and facilitate seamless integration into existing production lines.
- Russia: Dairy and supplement manufacturers in Moscow and Siberia operate our SS316L protein powder mixers and milk powder blenders in extreme cold conditions, with insulated jackets and heated CIP circuits ensuring year-round reliability.
- Arab Food Markets: Food producers in Saudi Arabia, the UAE, and Qatar rely on our dust-free ribbon mixers for halal-certified spice blends, instant soup mixes, and nutritional supplement production. All units meet GCC food safety standards and feature stainless steel construction resistant to high ambient temperatures.
Whether you are expanding a local production facility or establishing a new food processing plant, our team provides complete turnkey solutions — from initial consultation and custom engineering to installation supervision and after-sales support. Visit our contact page to discuss your specific requirements.
Frequently Asked Questions
What is the difference between a regular ribbon mixer and a food grade ribbon mixer?
A regular ribbon mixer is designed for general industrial powders and may use carbon steel or untreated stainless steel. A food grade ribbon mixer is constructed entirely from certified SS304 or SS316L stainless steel on all product-contact surfaces. It features polished internal welds, sanitary gaskets, CIP-ready spray systems, and dust-tight seals to prevent contamination — meeting FDA, EU, and GMP food safety requirements.
Can a food grade ribbon mixer handle wet and dry ingredients together?
Standard ribbon mixers excel at dry-to-dry blending. For formulations containing liquid binders or moisture above 5%, a paddle mixer or ploughshare mixer may be more suitable. However, our food grade ribbon mixers can accommodate up to 3% liquid addition (such as anti-caking oil or flavoring agents) using precision spray nozzles mounted on the mixer lid.
How often should a CIP mixer be cleaned?
Best practice in food processing dictates cleaning between every product changeover and at the end of each production day. Automated CIP cycles reduce cleaning time to 45–90 minutes and ensure repeatable results. For high-risk allergen changeovers (e.g., switching from nut-containing to nut-free protein powder), a validated CIP cycle followed by swab testing is recommended.
What mixing uniformity can I expect?
Our food grade ribbon mixers achieve a coefficient of variation (CV) of less than 3% for dry-to-dry blends, well within the ±5% tolerance required by most food industry standards. For challenging formulations with wide density differences — such as blending 1% flavoring into 99% carrier powder — optimized ribbon geometry and longer mixing times ensure uniform distribution.
Do you provide installation and training services overseas?
Yes. We dispatch experienced engineers to client sites in Spain, Russia, the Arab world, and other international markets for installation supervision, commissioning, operator training, and preventive maintenance. Remote troubleshooting via video link is also available for all customers worldwide.
Conclusion
Selecting the right food grade ribbon mixer is a critical decision that impacts product quality, regulatory compliance, and operational cost. Shanghai Deyue Machinery delivers SS304 and SS316L ribbon blenders engineered for the highest food safety standards — featuring CIP clean-in-place systems, dust-free sealing, and proven performance in flour, spice, protein powder, milk powder, and sugar processing applications.
With decades of manufacturing expertise and a growing global footprint across Europe, Russia, and the Middle East, we partner with food producers who demand reliability, hygiene, and efficiency. Explore our DLH Large Scale Ribbon Mixer range or reach out through our contact page to discuss a customized solution for your food processing facility.
Contact Us:
Phone: +86 13917895463
Email: [email protected]
Website: https://www.deyuemixer.com/
label:
related news